
Newsroom
Closure processing: how to tell if stopper preparation is limiting your filling line
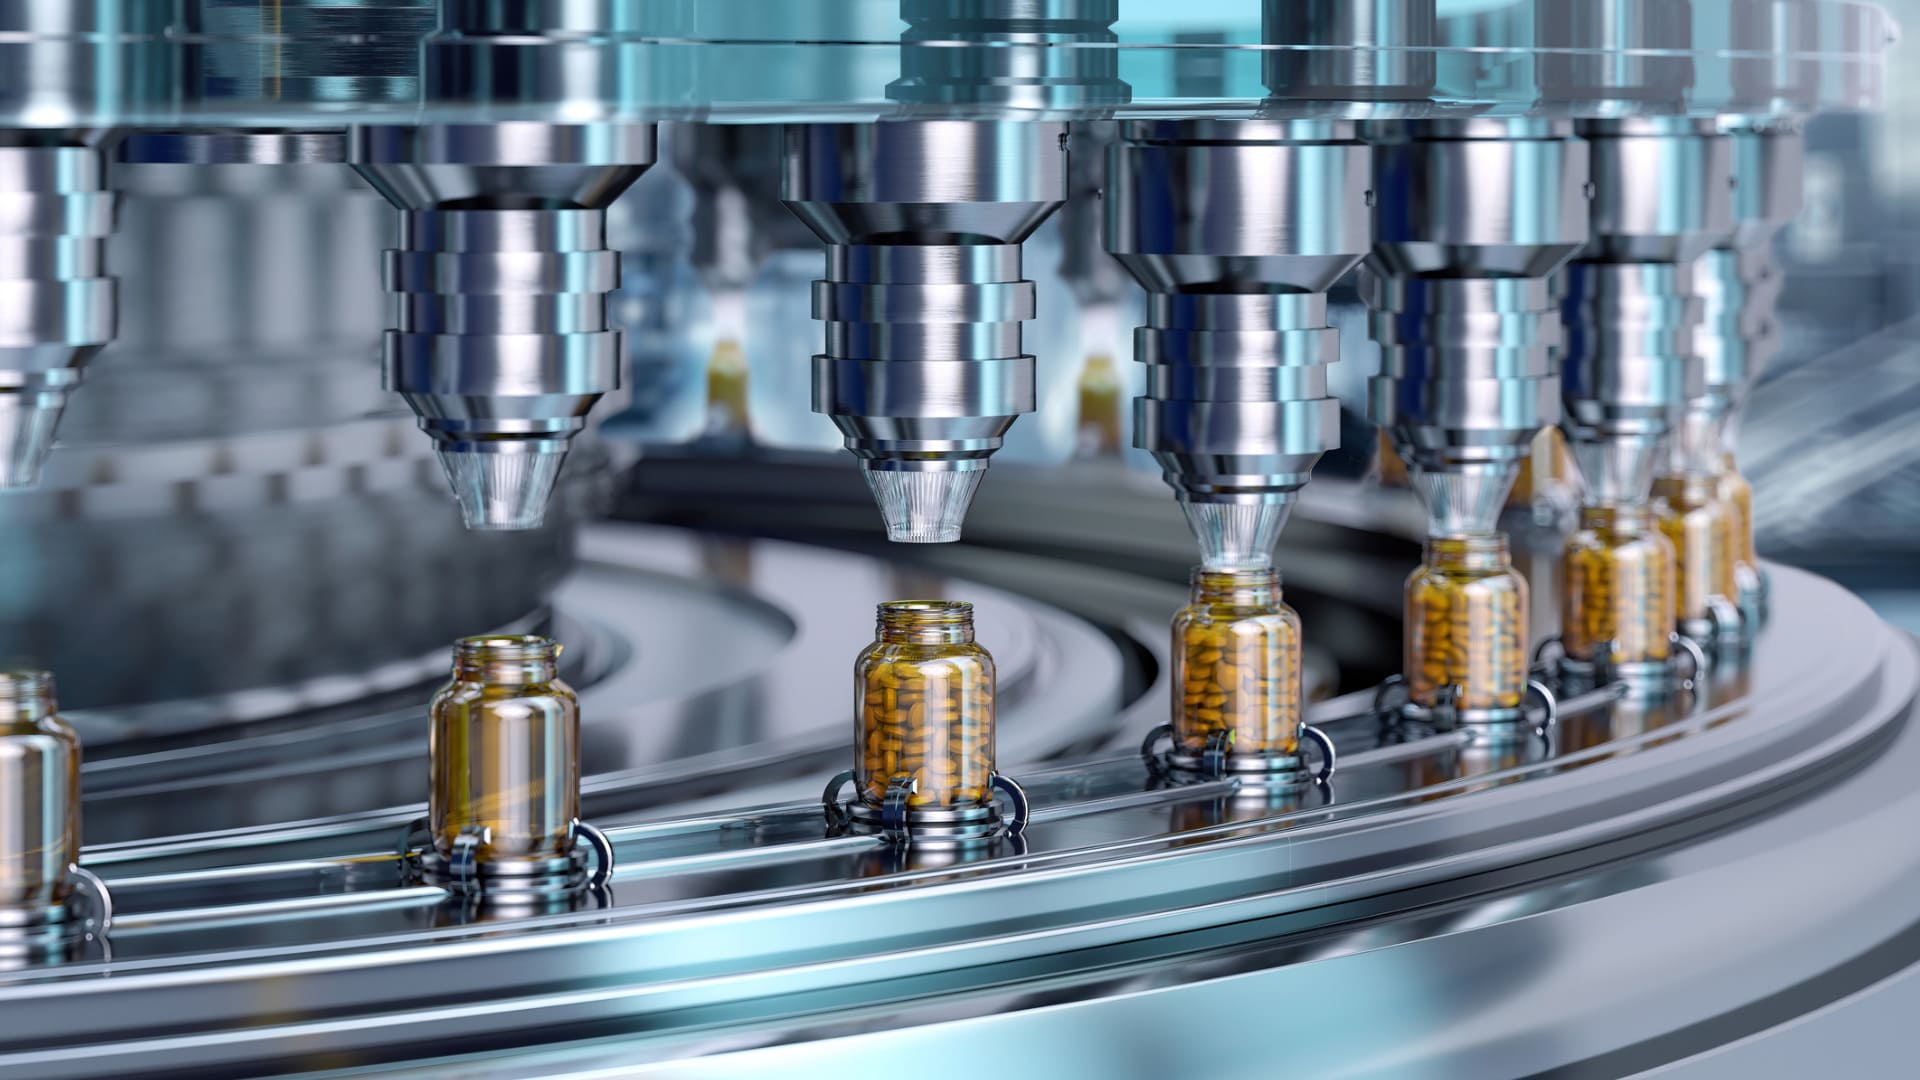
Closure processing becomes a capacity constraint when batch size and cycle time stop matching what the filling line consumes. Rubber stoppers, syringe plungers, gaskets and seals go through washing, rinsing, siliconization, sterilization and drying, and each of those stages affects process duration, particulate and endotoxin control, and residual moisture on the components.
This article is written for production and engineering teams in pharmaceutical manufacturing. It covers how to measure whether stopper preparation is actually the bottleneck, which stages cycle time builds up in, where you can intervene, and how in-house processing compares with buying ready-to-sterilize or ready-to-use closures.
Why closure preparation can limit a filling line
A closure destined for a parenteral product has to reach the capping machine clean, with particulate and endotoxins under control, sterile, and with residual moisture within specification. Several stages in sequence are needed to get there, and each one carries quality constraints that prevent it from simply being shortened.
The constraint comes mainly from a difference in rhythm:
- the filling line consumes closures continuously, at a rate set by the format and the product
- component preparation works in batches, with a fixed cycle time and a maximum load capacity
- between the two there are hold times and transfers: loading, unloading, packaging, passage into the aseptic area
If the number of conforming closures produced in a shift falls below what the filling line requires, the line can stop for lack of available components. The problem is not always visible directly: it can show up as short stoppages, batches of closures prepared in advance and held for long periods, or cycles made more conservative than necessary to compensate.
How to confirm that closure preparation is the bottleneck
Measure before changing the process. The baseline comparison is between how many conforming closures preparation makes available over time and how many the line consumes in the same period.
Calculating effective capacity
Effective preparation capacity is calculated as follows:
effective capacity = conforming closures per batch / total time per batch
Total time per batch is not the same as machine cycle time. It has to include loading, unloading, packaging, transfer into the aseptic area and hold times between stages. Using cycle time alone overstates available capacity.
Compare the result with the filling line’s closure consumption per hour or per shift, allowing for rejects and format changeovers.
Worked example with hypothetical figures, not referred to specific machines: if a batch yields 30,000 conforming stoppers and takes 6 hours in total including cycle, handling and hold times, effective capacity is 5,000 stoppers per hour. A line consuming 6,000 per hour will run short, even though machine cycle time on its own would appear sufficient.
KPIs to collect
To find where capacity is lost you need data by stage, not just the total:
- overall cycle duration (washing, rinsing, sterilization and drying)
- residual moisture at end of cycle against specification
- quantity processed per batch and reject rate
- format changeover time and changeover frequency
- filling line stoppages caused by closures not being available
If line stoppages for missing closures are rare and effective capacity exceeds consumption with margin, the bottleneck is elsewhere. In that case optimizing closure preparation will not increase output.
Where cycle time builds up
The table supports the KPI review: for each stage it gives the signal that points to a bottleneck, the variables to control, and the effect on the process.
| Stage | Bottleneck signal | Variables to control | Effect on the process |
| Washing | Long or repeated cycles | Load configuration, water quality, detergent use | Longer cycle time |
| Rinsing | Difficulty meeting final criteria | Final rinse water quality, number of repetitions, end-of-rinse criterion | Longer cycle time |
| Siliconization | Batch-to-batch variability, jams in the capping machine | Silicone quantity and distribution | Line stoppages, particulate risk |
| Sterilization | Difficult heat penetration into the load | Load arrangement, temperature, exposure time | Cycles more conservative than necessary |
| Drying | Residual moisture out of specification | Load geometry, drying method (hot air, vacuum or a combination, depending on the load), time | Delayed unloading |
| Transfer | Many manual manipulations | Packaging type, method of passage into the aseptic area | Time and contamination risk |
| Format changeover | Frequent or lengthy setups | Per-format recipes, load configuration | Loss of available capacity |
Endotoxins and rinsing
For rubber closures, endotoxin reduction is normally handled through validated washing and rinsing processes rather than the dry heat depyrogenation used for glass. The FDA aseptic processing guidance points to final rinses with water for injection (WFI) for parenteral products and requires washing validation to demonstrate endotoxin removal. Cutting rinse steps shortens the cycle but reduces the margin against that requirement.
Sterilizing a load of rubber components
Rubber is a poor heat conductor, so heat penetration into a load of stoppers deserves particular attention during validation. A dense or poorly arranged load forces longer cycles to guarantee conditions at every point. Cycle development principles are the same ones described in the guide to cGMP autoclave sterilization cycles, with the difference that here the load consists of thousands of small components in contact with one another.
Load configuration has a direct effect here. CPE and CPE-W processors from LAST Technology divide closures across several baskets rather than treating them as a single mass: splitting the load distributes it more evenly and exposes a larger share of component surface both to the wash solution and to steam during sterilization.
Drying and residual moisture
Material, formulation, closure geometry and load configuration determine how much moisture has to be removed after washing and steam sterilization. Drying is often one of the heaviest stages in the cycle: it can account for roughly half of total duration when the residual moisture target requires extended times. The FDA guidance notes that residual moisture on stoppers can support microbial growth and endotoxin formation, and for that reason recommends minimizing the time between washing, drying and sterilization. For some products, lyophilized ones in particular, closure moisture also matters for product stability.
| Is closure preparation a bottleneck on your line? Send us your closure types, batch quantities, line consumption and aseptic area configuration, and our technical team will help you identify the stage where capacity is lost. |
Where to intervene
Once the data confirms that the constraint is in preparation, the most effective changes act on load organization and process design before they act on the duration of individual stages.
Organize the load evenly
A compact, uneven load slows every stage: water circulates less freely, heat penetrates more slowly, drying proceeds unevenly. Distributing closures evenly reduces build-ups and impacts between components, which affects cleanliness, particulate and cycle repeatability.
This is the principle behind the multi-basket load arrangement used on CPE and CPE-W processors: splitting closures rather than treating them as a single mass stops them compressing against each other and increases the surface reached by the wash solution.
Dedicated recipes per closure type
A single cycle sized on the most difficult closure penalizes all the others. Separate recipes by material and format avoid oversizing rinse and drying steps where they are not needed, and shorten changeover times. It follows the same logic as customized pharmaceutical machinery, where the process is built around the actual load.
Controlled, repeatable siliconization
Siliconization reduces friction between closures and helps them feed into the capping machine. The process nonetheless has to be controlled, so that silicone distribution stays uniform and component and product quality requirements are met.
Reduce hold times between stages
Hold times may sit outside machine cycle duration, but they affect effective capacity and can affect process quality as well. Residual moisture that is not adequately controlled, combined with extended hold times, can increase microbiological risk, depending on process and storage conditions. Integrating washing, drying and sterilization into a continuous sequence, or at least defining validated maximum hold times, improves throughput and control together.
Fewer manipulations during transfer
Every manipulation between unloading and the line adds time and risk. Unloading closures directly into a sealed sterile package and reducing manipulations during transfer into the isolator, for example through RTP systems compatible with the process, can cut both operating time and contamination risk.
What EU GMP Annex 1 and the FDA guidance require
For manufacturers supplying the European market the main reference is EU GMP Annex 1 on the manufacture of sterile medicinal products, in the revision published in 2022 and effective from 25 August 2023. Several points bear directly on closure preparation:
- validated component cleaning (§ 8.2): primary packaging containers and components must be cleaned using validated processes that keep particles, endotoxins and bioburden under control
- preparation as an aseptic process (§ 8.12): opening, assembly and preparation of sterilized components in direct or indirect contact with the product must be treated as an aseptic process, in grade A with a grade B background
- unidirectional transfer (§ 4.11): components enter grade A or B areas through a unidirectional flow, sterilized in place where possible; where that is not possible, validated equivalent methods are required, such as rapid transfer systems for isolators
- protection after sterilization (§§ 8.46-8.48): sealed and qualified packaging, defined maximum hold times before and after sterilization, verification of sterile barrier integrity before use, assessment of rapid transfer ports
For manufacturers exporting to the United States, the FDA guidance Sterile Drug Products Produced by Aseptic Processing, issued in 2004, is also relevant; it is a non-binding recommendations document. On rubber closures it points to final WFI rinses, validation of endotoxin removal, reduced time between washing, drying and sterilization, attention to heat penetration, and silicone quality control. The two documents are not equivalent and apply according to the destination market.
RTS and RTU: in-house processing or pre-processed closures?
Part of the preparation can be moved outside the plant by buying closures that have already been treated. That choice changes the shape of the bottleneck, but it does not remove the responsibilities of the company manufacturing the drug product.
Definitions
- RTS, ready to sterilize: closures already washed through a validated process, optionally siliconized, and packaged, which still have to be sterilized before use
- RTU, ready to use: closures washed, packaged and already sterilized, ready for introduction into the line
The same abbreviations also describe the output state of an in-house process: a preparation system can take closures as far as the RTS state or as far as the RTU state.
RTS vs RTU: what actually changes for the manufacturer
The difference between the two is one stage. RTS closures arrive washed and packaged and still have to be sterilized on site, so the sterilization cycle and its validation stay in-house. RTU closures arrive already sterile and go straight into the line, so no treatment stage is performed on site at all.
What does not change is responsibility. In both cases the drug product manufacturer has to qualify the supplier and review the validation behind the state being claimed, and in both cases hold times, packaging integrity and transfer into the aseptic area remain its own process steps.
Three operating models compared
| Model | Stages performed in-house | Strengths | Points to weigh |
| Full in-house processing | From washing to drying, through to the RTU state | Direct control of parameters, format flexibility, less dependence on supply | Investment, floor space, validation and process management carried by the company |
| Buying RTS closures | Sterilization and drying where required | No in-house washing, shorter cycle | Unit cost, supplier qualification, sterilization still to be validated |
| Buying RTU closures | Transfer and introduction into the line only | No in-house treatment, simpler day-to-day operation | Unit cost, lead times, availability of special formats |
Outsourcing does not transfer responsibility
Buying pre-processed closures does not remove the obligation to verify the process. The FDA guidance states that third-party facilities sterilizing or depyrogenating containers and closures are subject to the same cGMP requirements as in-house treatment, and that the drug product manufacturer must review the supplier’s validation protocol and report. Audits, supplier qualification and incoming controls therefore belong in the cost comparison.
When in-house closure processing makes sense
No model is better in absolute terms. In-house processing tends to suit situations where:
- volumes are high and continuous, and the unit cost of pre-processed closures outweighs the investment in a system
- formats are numerous or special, and dedicated recipes are needed that a standard supplier does not always offer
- the product has tight requirements on silicone, residual moisture or extractables, and cycle parameters need to be controlled directly
- continuity of supply is critical, and dependence on external lead times needs to be reduced
RTS or RTU closures are worth weighing carefully where volumes are modest, formats are standard and cleanroom space is limited.
For in-house processing, the CPE and CPE-W pharmaceutical closure processors from LAST Technology cover washing, rinsing, siliconization, drying and cooling. The CPE-W runs the treatment without the steam sterilization stage and takes the load to the RTS state, while the CPE also integrates saturated steam sterilization and can take the load through to the RTU state.
To assess your own case with process data in hand, get in touch.
Technical references
European Commission, EudraLex Volume 4, EU Guidelines for Good Manufacturing Practice for Medicinal Products for Human and Veterinary Use, Annex 1: Manufacture of Sterile Medicinal Products, C(2022) 5938 final, 22 August 2022, effective from 25 August 2023. Official document (accessed 16 September 2026)
U.S. Food and Drug Administration, Guidance for Industry: Sterile Drug Products Produced by Aseptic Processing, Current Good Manufacturing Practice, September 2004. Official document (accessed 16 September 2026)
FAQ - Frequently asked questions
Compare effective preparation capacity, that is conforming closures per batch divided by total time per batch including handling and hold times, with filling line consumption over the same period.
Related posts
mail
Subscribe to our newsletter
Stay up to date with the latest news from LAST Technology